Every time a lab reactor system is opened, whether to load catalyst, replace a reactor tube, or change out a fitting, it has to be leak tested before it goes back into service. Over 13 years of designing, building, and operating lab reactor systems, the test I relied on for that was a pressure-decay hold: block the system in with an inert gas, watch the pressure, and decide whether the loss is acceptable.
The last part is where people differ. Ask experienced reactor people what leak rate is acceptable and many will start with zero. That is the right goal, but no assembled system holds zero, and a criterion nobody can meet does not help you decide whether to start a run.
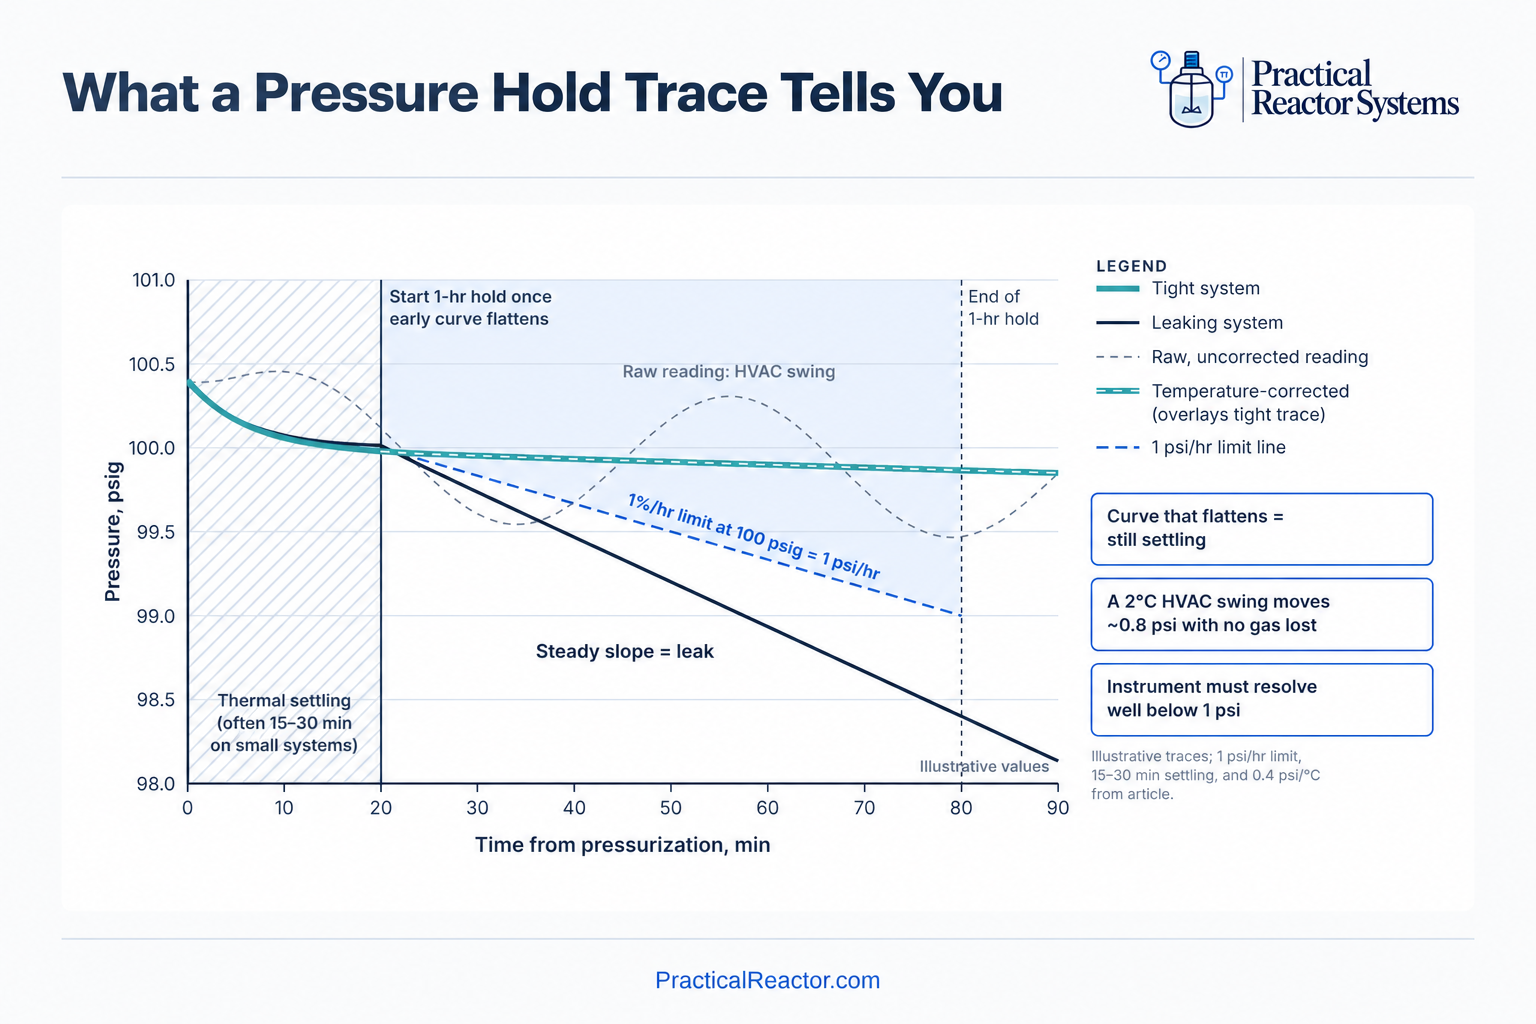
The criterion I used, and the one that held up on the small lab systems I worked with, was no more than 1% of test pressure per hour, temperature-corrected, over a one-hour hold. At 100 psig, that is a loss of no more than 1 psi in an hour.
I did not come up with that number. Across the four sites and two companies I worked at, most of the experienced reactor people I worked with used it, and most of the rest used something closer to 2%. It is not written in any code that I know of. The first part of this article covers the test conditions that make the number meaningful. The second part covers why I think the criterion settled where it did, and what it does and does not protect against.
Scope: This article covers routine leak checks of assembled laboratory reactor systems, typically small tubing-and-fitting units built from Swagelok-type components. It is not a pressure-rating, proof, or code test. It assumes every component is rated for the service and any required testing has already been completed, and the test pressure should never exceed the rating of the lowest-rated component. It also does not replace a hazard analysis. Where your site has an approved leak-test procedure, follow it.
The Test Conditions Matter More Than the Number
A leak-rate criterion means very little without the conditions it was measured under. The same 1 psi loss can describe a tight system or a leaking one depending on how the test was run.
Test Cold
When you load catalyst, replace a reactor, or break into process tubing, the system is cold. The heat tape and insulation are off and the furnace has cooled, because that is the only practical way to work on it. Once everything is back together, there can be a temptation to heat it up before testing, since that is where it will operate. For routine turnaround work, I would test it cold first.
The practical reason is time. If you heat the system and then find a leak, you have to cool it down, repair it, retest it, and heat it back up. A twenty-minute fix can take most of the day.
Cold testing is also a reasonable baseline for many of the seals on lab reactors. PTFE expands considerably more than stainless steel, so in PTFE-packed valves and similar seals the first heat-up can increase seal compression rather than reduce it. That does not mean a system that holds cold will hold hot. Thermal gradients, differential expansion between materials, tubing movement, gasket relaxation, and repeated thermal cycling can all open leaks that were not there during the cold test. A passing cold test is the first check, not proof that the system will stay tight at temperature.
PTFE also creeps under compression, so a packing or joint that was tight before its first heat cycle may behave differently after several. The cold test before run twenty is not necessarily the same test as the cold test before run one, which is one reason to keep a record of each result. I come back to that at the end.
Test at Operating Pressure
Test at the pressure the system will actually see in operation. Testing well below it can make a leak look much smaller than it will be in service. For an idealized laminar leak through a small channel, gas leakage scales roughly with the difference of the squares of the absolute pressures. By that relationship, testing a 100 psig system at 50 psig understates leakage by a factor of about three, not two.
If the available inert-gas supply limits your test pressure, record the pressure you actually tested at and treat the result as a lower-pressure test rather than an equivalent one.
Also watch the relief device. If the system is tested at operating pressure and the relief is set only slightly above it, a soft-seated relief valve can start to simmer well below its set point, sometimes around 90% of set. That shows up as a steady pressure decay that no bubble check will find, because the gas is leaving through the vent line. If a hold test fails and every accessible joint checks clean, the relief path is one of the first things to rule out.
Correct for Ambient Temperature
Temperature is the condition most often left out of informal testing, and its effect can be large enough to swamp the measurement.
For a blocked-in volume of gas, absolute pressure moves in proportion to absolute temperature. At 100 psig, the absolute pressure is about 114.7 psia, and near room temperature a 1°C change moves the reading by roughly 0.4 psi. If the lab swings 2°C over an HVAC cycle, the pressure can move almost 0.8 psi without any gas leaving. Against a 1 psi criterion, an uncorrected test may be measuring the building more than the reactor.
Log temperature along with pressure and correct each reading to a reference temperature:
P corrected = P measured × (T reference / T measured)
Pressure and temperature both have to be in absolute units, psia and K or °R. The correction does not work with psig and °C.
Ambient temperature is also only a stand-in for the gas temperature. If the reactor or nearby equipment is still settling, the gas will lag the room. That is one more reason to look at the shape of the pressure trend rather than only the starting and ending values.
Let the System Reach Thermal Equilibrium
Do not start the one-hour hold the moment the system is pressurized. Compressing gas quickly into a small volume heats it, and as it cools back toward room temperature, the pressure falls in a way that looks exactly like a leak.
On many small systems, 15 to 30 minutes is enough, but the pressure trace is a better guide than the clock. Start the hold once the early, rapid part of the curve has flattened out.
Log the Pressure Through the Hold
Record pressure continuously through the hold rather than reading a gauge at the start and end. Two readings tell you how much pressure was lost. A logged trend also shows the shape of the loss. A drop that gradually flattens is usually the system still settling, while a steady downward slope is a leak.
Before relying on the instrument, make sure it can resolve the change you are looking for. A test against a 1 psi criterion needs a reading good to a small fraction of a psi. A coarse Bourdon gauge cannot do that, and a wide-range transducer read through a low-resolution input may not either. If the readout cannot resolve well below the acceptance limit, the test cannot tell a pass from a fail.
Block In the Section You Worked On
One of the most useful design features on a lab reactor system is an isolation valve close to each connection that gets opened routinely, typically just upstream and downstream of the reactor.
The reason is sensitivity. Pressure-decay sensitivity depends heavily on the volume being tested. If the full process system holds 1000 cc of gas but the reactor section you opened holds 150 cc, the same leak produces roughly seven times as much pressure drop in the smaller section. The leak is no bigger and the measurement is no more careful. The box is just smaller, which makes small leaks much easier to see.
It also helps the rest of the system. If the remaining equipment stays blocked in under inert pressure while the reactor section is open, less of the system needs to be repurged and less surface is exposed to air. There is also little value in retesting several feet of untouched tubing every time a reactor is replaced, so the isolation points should sit reasonably close to the connections being disturbed.
The isolation valve then becomes part of the test boundary, and its seat leakage becomes part of the measurement. Soft-seated valves can provide very low seat leakage, but a soft seat does not guarantee a tight valve, and a metal seat does not mean the valve leaks significantly. Check the actual seat-leakage specification.
Internal Leakage Looks the Same as External Leakage
The transducer only knows that gas left the blocked-in volume. It cannot tell whether the gas went out through a fitting or across a valve seat into a lower-pressure or vented section. A needle valve seat, a soft-seated check valve, or a three-way valve passing to a vent line all produce the same trace as a leaking union.
When a section fails the hold and a careful bubble check of every joint comes up clean, checking the same fittings again is rarely productive. Subdivide the volume with block valves and test the pieces separately. In that situation, the cause is usually a valve seat rather than a connection.
The Test Gas Is Not Always the Process Gas
Most reactor systems are leak tested with nitrogen or another inert gas, and the process gas can behave differently. Hydrogen is the important example, and there are two separate effects to consider.
Leakage Through an Actual Leak Path
In viscous flow, leakage depends on gas viscosity. Near room temperature, nitrogen is about 18 µPa·s and hydrogen about 9 µPa·s, so hydrogen could pass through the same leak path at roughly twice the nitrogen rate. In molecular flow, leakage depends on molecular mass instead, and the ratio is about 3.7, the square root of 28/2.
Real fitting leaks are neither perfect capillaries nor pure molecular-flow orifices, and they can shift between regimes as the joint moves. So the useful conclusion is not a specific hydrogen number. It is that a nitrogen test can be optimistic for hydrogen service by something like a factor of two to four. That is one of the reasons I prefer 1%/hr over 2%. Once you convert to hydrogen, the looser number does not leave much margin.
Permeation Through Seal Materials
Permeation is a different mechanism. Gas can dissolve into a polymer seal and diffuse through the material itself, with no mechanical gap involved. It does not follow the leak-path relationships above. It depends on the specific gas, polymer, temperature, pressure, and geometry, and hydrogen permeates PTFE and elastomers very differently from nitrogen.
A nitrogen pressure-decay test cannot detect hydrogen permeation, and no correction factor fixes that. It has to be handled through valve and seal selection, minimizing unnecessary polymer sealing surfaces where practical, hydrogen detection, and following the site’s procedure for introducing hydrogen into a new or disturbed system.
Where Helium Fits
Helium is sometimes recommended as a stand-in for hydrogen because it is a small molecule. That is only partly true. In molecular flow it is closer to hydrogen than nitrogen is, but in viscous flow its viscosity is slightly higher than nitrogen’s, which makes it a worse stand-in in that regime.
Helium’s real advantage is detectability. A helium leak detector can find extremely small leaks and show you where they are. That changes the problem from “the transducer says something is leaking” to “it is this union,” which is a very different troubleshooting job. For systems where very low leakage matters, that makes helium testing worth doing even though helium is not a perfect physical substitute for the process gas.
Why 1% and Not 0.1% or 5%?
If 1% is not in a code, it is fair to ask why so many people ended up there. My explanation is that for a routine build-quality check, the criterion is set by whether you can find the leak, not by the hazard limit.
The numbers line up closely. A 150 cc blocked-in section losing 1 psi in an hour is leaking about 2.8 × 10⁻³ atm·cc/s, or roughly 245 cc per day at atmospheric conditions. Bubble leak-detection solutions are generally good to somewhere around 10⁻³ to 10⁻⁴ atm·cc/s under good conditions. The acceptance criterion sits right at the detection limit of the method most people use to locate leaks.
That relationship matters in both directions. If the criterion is set well below what you can locate, the system fails, you know something is leaking, and you cannot find it. Someone spends two hours checking every fitting, finds nothing, and eventually runs the unit anyway because “it always does that.” A criterion that gets routinely set aside stops functioning as a criterion. If it is set well above what you can locate, you are accepting defects you could have found and fixed in twenty minutes.
So the principle behind the 1% rule is to set the routine criterion at a level that catches meaningful assembly problems while still giving the person troubleshooting a reasonable chance of finding them.
This also gives the 2% group more credit than it usually gets. A percentage pressure decay does not account for volume. A 1% loss from 1000 cc is far more gas than a 1% loss from 150 cc, so someone testing a whole unit at 2%/hr may be holding a tighter physical standard than someone testing an isolated reactor section at 1%/hr. The practical fix is to record the approximate isolated volume alongside the allowable decay. With both numbers, the criterion means the same thing from one system to the next and from one person to the next.
What the Criterion Protects
For the small blocked-in volumes discussed here, 1%/hr will usually be well inside what a properly designed, ventilated enclosure can handle. That does not make it a safety limit. The allowable release for a particular system has to come from the hazard analysis: gas composition, toxicity, flammability, operating pressure, inventory, enclosure volume, ventilation rate and reliability, detection, ignition sources, and failure scenarios.
What the 1% criterion does well is catch problems before they turn into operating problems. Three are worth calling out.
Data Quality
On a continuous reactor with mass flow controllers setting the feed and a GC closing the material balance, a leak is an unmetered flow path. It usually does not cause an alarm. It shows up as a mass balance that never quite closes or a conversion that is consistently off, and it is possible to collect weeks of data before realizing the reactor was never running at the conditions you thought it was.
Catalyst Bed Integrity
A path that lets gas out under positive pressure can let air in during a cooldown or any excursion below atmospheric pressure. For a reduced or air-sensitive catalyst, a small leak can ruin a run without ever becoming a personnel hazard.
Build Quality
Most leaks have a specific cause: a fitting that was not made up correctly, a ferrule reused one time too many, valve packing that needs attention, a damaged gasket surface, or a connection disturbed during a reactor change. On a system where most of the joints disappear behind insulation and enclosure panels as soon as it is closed up, the leak test is the one step that makes you check your own work before the run starts.
That last one is the strongest argument for the criterion. It is a build-quality check, and sitting well inside the hazard limit is part of what makes it useful. A criterion set at what the enclosure can tolerate would pass a system that is coming apart.
Higher-Consequence Service
For gases with low exposure limits, unusual toxicity, or other high-consequence properties, the general 1% rule should not be applied automatically. Determine the allowable leak rate from the hazard analysis, then confirm that the test method can detect leakage comfortably below it. The routine 1% criterion is a build-quality rule, not a substitute for a consequence-based limit where one is needed.
Track the Results Over Time
If the decay result is recorded each time the system is opened, each reactor section builds up a history, and that history turns out to be useful.
Most of the change in that history is slow and not worth chasing. Packing creep, valve wear, and normal aging produce gradual increases over many cycles, and the right response is to keep running until the section no longer meets the criterion.
A sudden change is different. If a section has tested around 0.3%/hr through six catalyst changes and then tests at 0.9%/hr, it still passes, but creep does not triple in a single cycle. Something changed, and at that moment you know exactly which connections were touched. The fix probably takes twenty minutes. If you wait until the section fails months later, you will no longer know where to look.
A jump that does not fit the established trend is worth investigating even when the test passes. That is the main reason to record the number instead of checking a box marked “pass.”
Final Takeaway
For routine leak checks on a small lab reactor system, the approach that worked for me was to test cold before heat-up, at operating pressure, on the smallest section that contains the disturbed connections. Let the system settle before starting the clock. Log pressure with an instrument that resolves well below the acceptance limit, log temperature alongside it, and correct using absolute units. Hold for an hour, accept no more than 1% of test pressure, and record the result along with the isolated volume so it can be compared against that section’s history. Where the process hazard calls for a tighter limit, derive it from the hazard analysis.
The leak test does not show that a reactor is safe. That comes from design, pressure ratings, materials, relief protection, ventilation, detection, procedures, and hazard review. The leak test answers a narrower question: whether the system was put back together well enough to trust before starting the run.